
High-Precision Automatic Grinding Solution for Key Components Such as Pump/Valve/Hydraulic Cylinder
Danobat is a company specializing in precision grinding and hard turning solutions. Next, I would like to introduce our products and cases in the hydraulic industry.
Introduction to Danobat
Danobat was established in 1954 and belongs to the Mondragon Group, a Fortune 500 company. Its product types are relatively complete, including small and medium-sized universal internal and external grinding machines, heavy-duty universal internal andexternal grinding machines, vertical grinding machines, and centerless grinding machines. At the same time, Danobat has acquired two world-class grinding machine companies, one is Overbeck from Germany, established in 1924, specializing in high-precision internal circular and arc grinding machines. Over the past 90 years, Overbeck has provided more than 9000 machine tools worldwide; Another company is Hembrug, located in the Netherlands. This brand has a high global reputation and specializes in producing ultra precision hard cars (which can be replaced by cars), car grinding composite centers, and vertical lathes. For more than 50 years, Hembrug has been a leader in ultra precision turning solutions. Danobat has provided precision solutions to over 3000 customers over the past 65 years; Danobat's annual revenue is 261 million euros, with over 1300 employees and 14 manufacturing factories worldwide, with most of its products exported. Most of the solutions provided by Danobat are customized according to customer needs. Our well-known clients in the hydraulic industry include Dr. Rexroth, Buchholz Hydraulic, Eaton Fluid, Ambiton, Grundfos,Clark, Leicester Ritz, Linde, Montebe, Sany, and Yuci Hydraulic. In other industries, such as Bauer, BHP Billiton, Bombardier, Daimler, General Electric, Heidelberg, Lufthansa, Rolls Royce, Siemens, American Steel, ZF, and others, we are all important customers.
Challenges in the hydraulic industry
The hydraulic industry is facing several challenges now. Firstly, environmental requirements are increasing, and there is an increasing demand for low energy consumption and efficient pumps; The second is the increasing demand for manufacturing accuracy; Thirdly, in terms of productivity, due to the wide variety of products in the hydraulic industry, there is an increasing demand for flexible solutions with fewer processing steps and simpler type changes; Fourthly, the dependence on human resources is decreasing.
Danobat has corresponding solutions for these challenges.For example, precision and high productivity centerless grinding machines can not only achieve cut in grinding but also achieve through grinding.
We use a natural granite bed for the internal grinding machine. The grinding wheel head frame is directly driven by a torque motor, which is the B1 axis. The workpiece head frame is also directly driven by a torque motor, which is the B0 axis. All of its linear shafts are directly driven by linear motors, without ball screw transmission pairs. The grinding wheel head frame can have one external grinding spindle and three internal grinding spindles. The inner hole, end face, and arc grinding can be completed in one clamping process, Very high flexibility.
The heavy-duty cylindrical grinding machine can even process workpieces with a length of up to 10m. There is a unique control on the heavy- duty cylindrical grinding machine, which is the Multi Diameter Measurement (MDM) system,which can achieve onlinemeasurement. It has a CNC axis and can measure wherever the grinding wheel is ground.
This is a high-precision Hemabrug hard car (see Figure 1), which uses full static pressure technology and has even higher accuracy than a grinding machine. This picture shows a secondhand Hemabrug lathe that has been in use for 17 years. After testing its workpiece head and spindle, the spindle's jumping still reaches 0.09 μ m. So the maintenance of machine tool rigidity and accuracy is very stable. In addition to the Hembrug hard car, we also provide a turning and grinding composite center, which means that external and internal grinding wheels can be added, and parts with special surface requirements can be turned first and then ground.
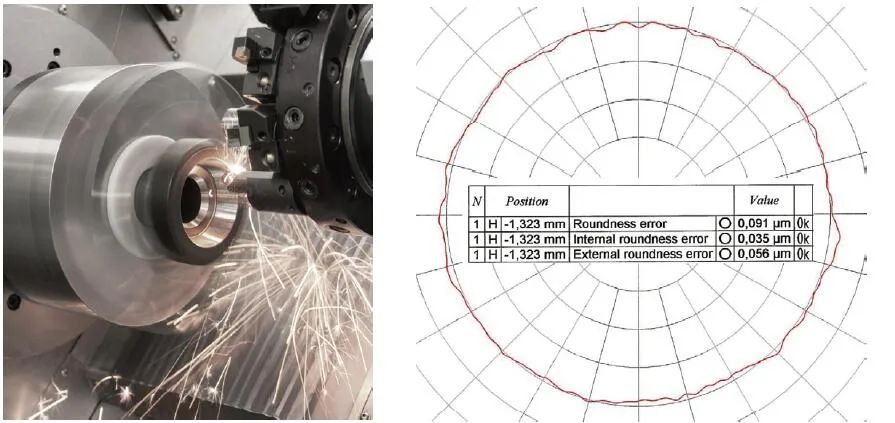
Figure 1 Hembrug's high-precision hard car
Cases in the hydraulic industry
Let's talk about application cases in the hydraulic industry, including gear pumps, plunger pumps, control valves, as well as some processing applications of other large hydraulic cylinders and hydraulic crushing hammers. This will mention heavy-duty cylindrical grinders, centerless grinders, small cylindrical grinders, and internal cylindrical grinders.
Plunger pump
The ball head plunger of the plunger pump is a typical workpiece, and we can use centerless grinding to process the plunger surface. Of course, in addition to centerless grinding, we can also use cylindrical grinding. We can install a polishing equipment on the cylindrical grinding machine, and the roughness can reach Ra 0.08 μ M (see Figure 2a).
We have corresponding solutions for the swash plate, sliding shoe, plunger, and port plate on the plunger pump. For example, the grinding of the inner spherical surface of the sliding shoe adopts a hydraulic eccentric indexing chuck, which can directly position the eccentric inner ball at the grinding position on the rotation center.
The valve plate is used to grind the outer spherical surface using an internal cylindrical grinder and the cup shaped grinding wheel is used for grinding.
This is a swashplate. We use a special fixture (see Figure 2b) to fix the two swashplates on a special fixture, and then use a double tip drive to grind the outer circle. This machine tool uses two CBN grinding wheels, one for coarse grinding and the other for fine grinding. Compared to traditional corundum grinding, using CBN grinding wheels can shorten the beat by 45% (see Figure 2b).
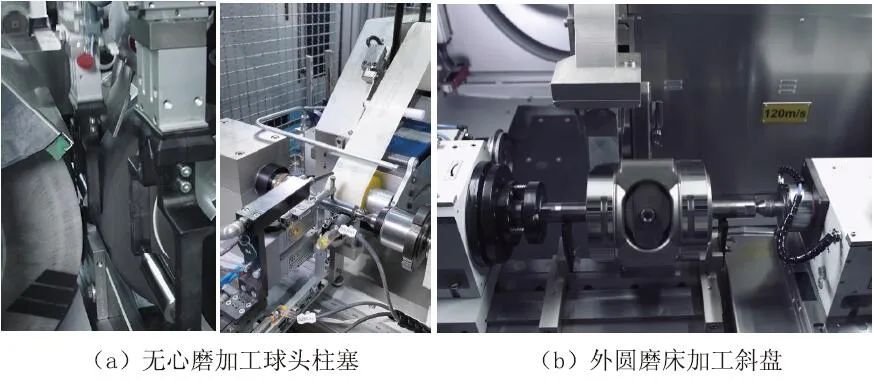
Figure 2 Case - Plunger Pump
Gear pump
The grinding position of the gear shaft is the outer diameter, cone surface, and end face on both sides of the gear. Double diameter online measurement is used, including a length measurement. During grinding, spiral lines are not allowed because of sealing requirements. Most can be efficiently ground using CBN grinding wheels, but ordinary grinding wheels can also be used (see Figure 3a).
The machining of gears is achieved on an internal cylindrical grinding machine, which grinds the inner hole, outer circle, and two end faces of the gears. We use two machine tools for online operation. One machine tool grinds the inner hole and one end face, while the other machine tool grinds the other end face (see Figure 3b).
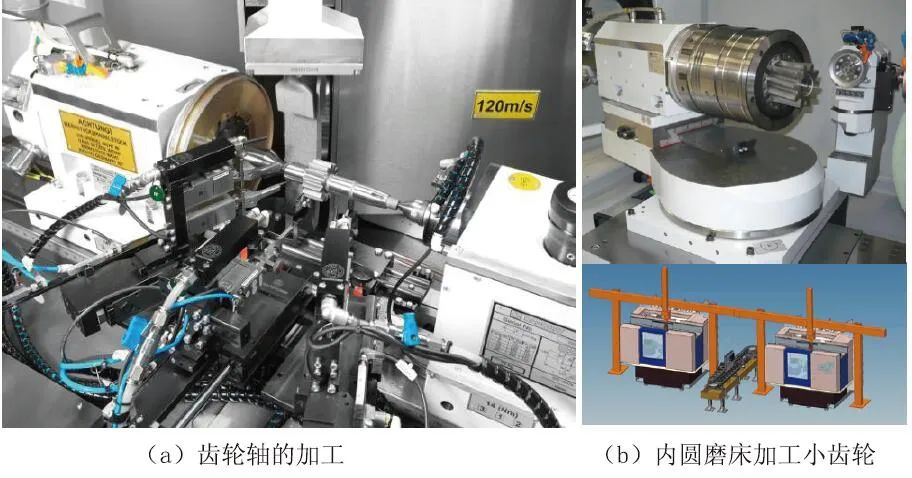
图3 案例——齿轮泵
Hydraulic fluid control valve
The valve core is processed on a centerless grinder, and there is a measurement system behind the line that can automatically measure and feedback dimensions, compensating for the next workpiece automatically. Even without measurement feedback, the accuracy of the machine tool itself can be guaranteed to be within 2 μ Within m (see Figure 4).
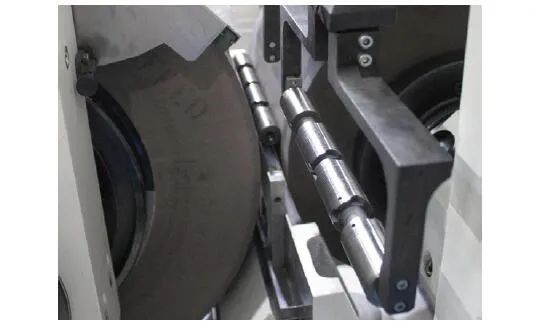
图4 无心磨床加工液压阀芯
For hydraulic valve cores with higher requirements, they can be machined using Hembrug's composite center, with a dimensional tolerance of 2 according to customer requirements μ m. Cylindricity 2 μ m. Roundness 1 μ m。 In the later batch production, the consistency of the workpiece can be controlled at 1 μ M (see Figure 5).
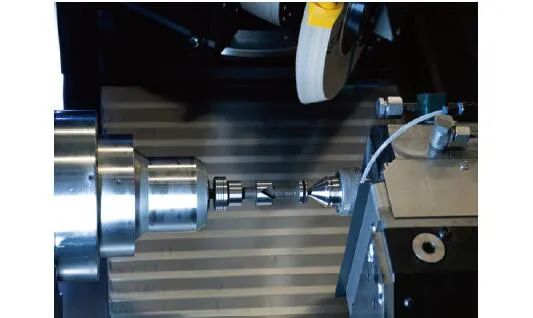
图5 复合中心加工更高要求的液压阀芯
The grinding of the hydraulic valve sleeve is completed using an internal grinder (see Figure 6), which requires the grinding of the front large hole, the grinding of the back small hole, and the grinding of the counterbore end face. This machine tool is multifunctional and multi-station, with one outer circular grinding wheel and three inner circular grinding wheels. In other words, one clamping can achieve grinding in all positions. Another highlight is that this machine tool can be equipped with a trimmer measuring device to detect whether the trimmer is worn.
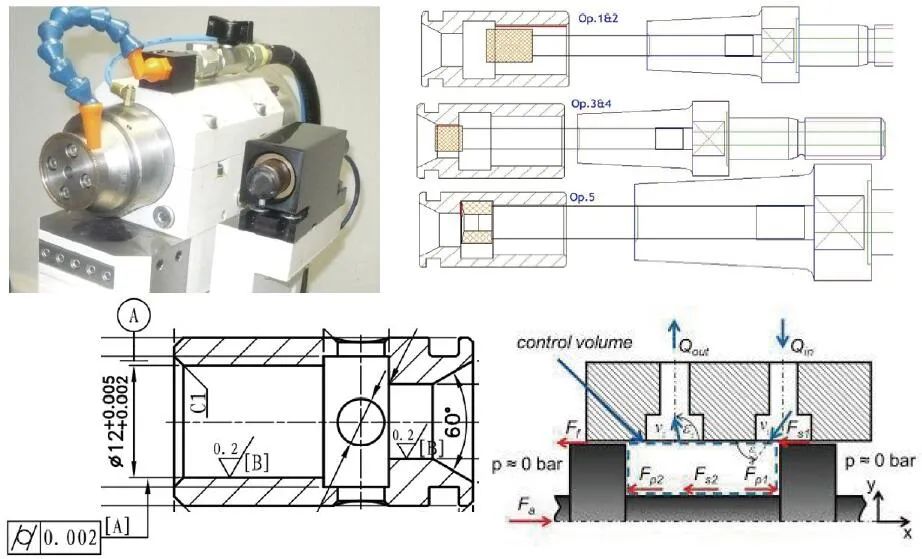
图6 内圆磨床加工液压阀阀套
This is the processing of a lift valve (see Figure 7), which is processed on an external cylindrical grinder with very high accuracy requirements. We use a high-speed CBN grinding wheel, which can achieve a linear speed of 140m/s.
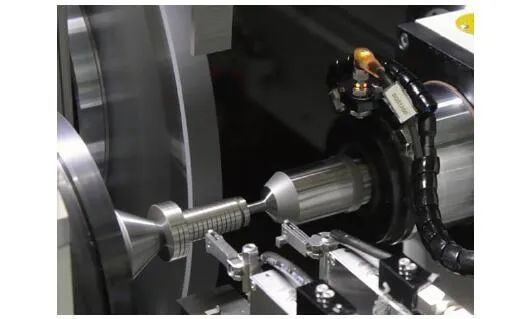
图7 外圆磨床加工提升阀
For grinding spherical surfaces and sealing surfaces, such as fixed ball valves, floating ball valves, and their valve seats, when grinding large spherical surfaces, the workpiece head frame can continuously swing to ensure the contour error of the spherical surface. For the sealing surface of the valve seat, we use an internal grinding wheel, which is ground using the generative method. This sealing surface usually has various coatings, such as sometimes coated with hard alloy, with a hardness of up to 90HRA. We use a diamond grinding wheel for grinding. In addition, our grinding machine can grind spherical surfaces and sealing surfaces, as well as both internal and external spherical surfaces. The traditional process is two machine tools, one for processing the outer spherical surface and the other for processing the inner spherical surface. However, we can achieve two functions with one machine tool (see Figure 8).
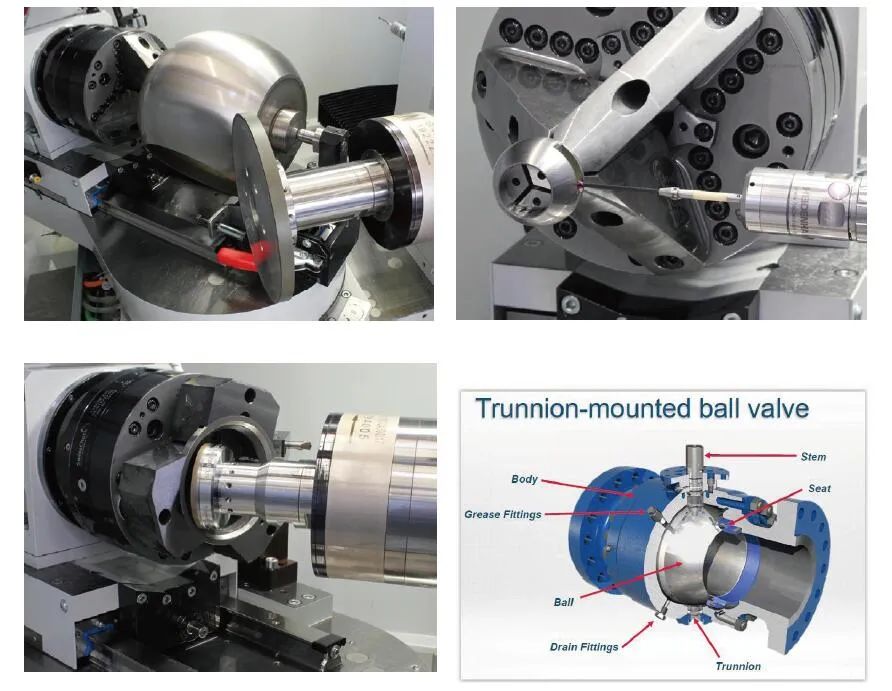
图8 内圆磨床加工固定 & 浮动球阀的球面和密封面